-
AboutHebei Daniu Environmental Protection Dust Removal Equipment Co., Ltd. was established in September 2006, always focusing on the research and sales of environmental protection equipment and accessories.

-
ProductsAlways focused on the research and sales of environmental protection equipment and accessories. Provide comprehensive environmental dust removal solutions, including but not limited to industrial dust removal equipment, air purification equipment, noise control equipment, etc.
-
BlogWe adhere to the principle of integrity first and customer first, and strictly control the quality of our products from the whole machine to the small parts. Always focused on the research and sales of environmental protection equipment and accessories.
Efficient Powder Transport: Exploring the Benefits of Bucket Elevators
26-09-30
Summary:
Bucket elevators are a vital component in the processing and handling of bulk powder materials across various industries. These devices are engineered to vertically lift materials using a series of buckets attached to a belt or chain. This design not only maximizes space utilization but also minimizes spillage and material degradation, making it an ideal solution for powder transport. One of the p
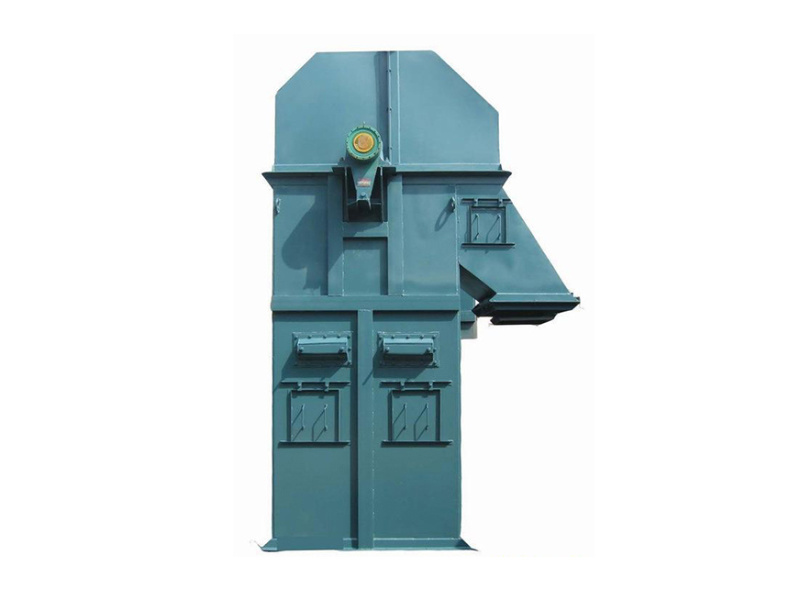
One of the primary advantages of bucket elevators is their ability to handle a wide range of powdered materials, including grain, cement, and food products. Their enclosed design helps to contain dust and prevent contamination, which is crucial when working with fine powders that can easily become airborne. Additionally, the vertical configuration allows for higher capacity transport in a smaller footprint compared to traditional conveyor systems.
When selecting a bucket elevator for powder transport, several technical considerations must be taken into account. The material of the buckets, for instance, must be compatible with the type of powder being transported to prevent wear and tear. Common materials include plastic, steel, or even stainless steel for applications requiring high hygiene standards. The bucket size and spacing also need to be optimized based on the characteristics of the powder—such as bulk density and flowability—to ensure efficient transport without clogging or bridging.
Another crucial aspect is the selection of the drive mechanism. Bucket elevators can be equipped with different drive systems, such as direct drive or gearbox-driven systems. The choice of drive affects not only the efficiency of transport but also the maintenance needs of the elevator. Regular maintenance checks are essential to ensure that the belts or chains remain tensioned and that the buckets are securely attached to prevent system failures.
In terms of operational efficiency, bucket elevators can be automated and integrated into existing production lines. This allows for seamless material handling processes, reducing the need for manual intervention and increasing overall productivity. Sensors can also be installed to monitor the elevator’s performance, alerting operators to potential issues before they escalate.
In conclusion, bucket elevators are an essential tool for the effective transport of powdered materials in industrial settings. Their ability to minimize dust, enhance efficiency, and integrate seamlessly into production processes makes them an invaluable asset. By carefully considering the specific needs of the powder being transported and ensuring proper maintenance, businesses can leverage the full benefits of bucket elevators for optimal performance in powder transport applications.
Previous page:


Contact Us
Cui Village, Fuzhen, Botou City, Cangzhou City, Hebei Province, China
Ask For A Quick Quote
We will contact you within one working day. Please pay attention to your email.